Hey there, if you’re in the business of making things that get sealed with HF (high frequency) welding—like inflatable rafts, PVC banners, medical drapes, or even car interior trim—you’ve probably asked yourself this question at some point: what’s the minimum thickness I can actually weld with an HF machine? As someone who’s been selling and supporting HF welding machines for the last 8 years, I can tell you this isn’t a one-size-fits-all answer. I’ve seen folks waste hundreds of dollars on underpowered machines because they picked the wrong minimum thickness, or struggle to get solid seals on super thin materials that should work. Let’s break this down like I would with a customer sitting across my desk, no tech jargon overload. HF Welding Machine
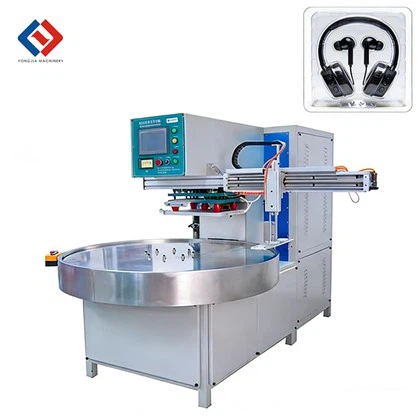
First, let’s get clear on what HF welding does, because that’s why thickness matters so much. Unlike traditional heat welding (where you press a hot bar against material), HF welding works by generating an electric field that excites the dipolar molecules in thermoplastic materials. Think PVC, PU, vinyl—materials that have molecules that line up positive and negative. When the high-frequency current hits, those molecules flip back and forth super fast, creating friction that heats the material from inside out. No external heat source means a way more even seal, which is why it’s perfect for flexible, thin stuff that would melt or burn with regular welding. But here’s the catch: that internal friction (and thus the heat) depends on how much of that electric field you can get inside the material. Thickness changes that game entirely.
Now, the minimum thickness isn’t just a number pulled out of thin air. It depends on three big factors: the type of material you’re welding, the power of your HF machine, and the type of seal you need. Let’s start with materials, because that’s the biggest variable. PVC is the most common for HF welding, right? Soft PVC (like the kind used for inflatable pool toys) is way thinner than rigid PVC. I’ve welded soft PVC as thin as 0.1mm before with a 1.5kW tabletop HF machine—those little keychain inflatable footballs? That’s exactly what we make. Wait, but rigid PVC (used for pipes, or some signs) is a different story. Rigid PVC doesn’t have as many dipoles, so you need way more material to generate enough heat. For rigid, the minimum I’d recommend is around 1mm, even with a good mid-powered machine.
Then there’s PU (polyurethane), which is super popular for outdoor gear and medical products. Flexible PU is similar to soft PVC—you can go as thin as 0.15mm with a 2kW machine, but if it’s a harder, thicker PU, you’re back to 1mm minimum. And if you’re welding something like TPU (thermoplastic polyurethane), which is even more stretchy, the minimum is still around 0.12mm for small parts, but you have to adjust your pressure to not stretch the material while it’s heating. I once had a customer try to weld 0.08mm TPU with a 1kW machine—he ended up with a seal that was so weak it ripped when he blew up his product. That’s why testing first is non-negotiable.
Next, machine power. That’s where so many people mess up. A lot of small business owners buy the cheapest HF machine they can find on Alibaba, thinking more power = better, but it’s actually the opposite for thin materials. A 1kW tabletop machine is perfect for thin stuff, but cranking it up to full power on 0.1mm material will burn a hole right through it. A 5kW heavy-duty machine, on the other hand, is for thicker materials—like 5mm vinyl for truck tarps—so if you try to use that on 0.1mm PVC, you’ll get uneven heat, partial seals, and wasted material. Let me give you a concrete example: last year, a guy from a custom sticker shop came to me. He was using a 3kW HF machine meant for large banners, trying to weld 0.2mm vinyl decals. He could never get a clean cut seal—either the edges burned, or the decal peeled off. We swapped him to a 1.2kW compact HF press, and he’s been cranking out perfect decals ever since. That’s a good rule: for materials under 1mm, stick to machines rated under 2.5kW. For 1-5mm materials, 2.5kW to 5kW is your sweet spot. For anything over 5mm, you’ll want 5kW or higher, but that’s rarely for small businesses.
Then there’s the seal type. Are you making a seam that needs to hold air (like an inflatable), or just a decorative edge that doesn’t need to be structural? If it’s a structural seam for something that will be under pressure, the minimum thickness goes up. For inflatables, I usually recommend at least 0.15mm—even if you can weld 0.1mm, that seam will get worn out fast when people are dragging the raft on concrete. If it’s just a PVC patch for a sign that won’t take any stress, you can go as thin as 0.08mm. Another thing: the size of your electrodes (the metal parts that apply the electric field) matters. Smaller electrodes (like for custom logos on decals) can focus the heat more, so you can go thinner. Larger electrodes (for long seams on banners) need a little more material to keep the heat consistent across the whole length.
Wait, let’s address a common myth I hear all the time: some people say “you can’t weld anything thinner than 1mm with HF machines.” That’s just not true. I’ve worked with thin films for medical device packaging—like 0.05mm PVC film for blister packs. We use a 1kW machine with a custom fine-tuned electrode, and the seals hold up to sterilization. But that’s a specialized setup, not a standard machine. If you’re a hobbyist or a small business, sticking to the general minimums is safer.
Now, what if you have material that’s thinner than your machine’s recommended minimum? Can you do anything to adjust it? Yeah, but it’s not ideal. First, you can add a sacrificial layer of a slightly thicker thermoplastic (like 0.1mm PVC film) between your thin material and the electrode. That way, the heat is spread evenly, and you don’t burn the thin stuff. Another trick is to lower the line speed (if you’re using a continuous roll HF machine) or the pressure on the press. Slower line speed means more time for the heat to set without burning, and lower pressure keeps the material from stretching or blowing out. But I’ll be honest: if you’re doing this regularly, it’s better to invest in a smaller, lower-power machine than to keep messing around with adjustments. It’ll save you time and material in the long run.
Let’s also talk about when thickness isn’t the only thing that affects this. Material quality matters too. Some low-grade PVC has fillers that make it harder to heat—so a 0.1mm cheap PVC might be impossible to weld, while a 0.15mm high-grade PVC works perfectly. I always tell customers to test their material with a sample machine before buying a full machine and a roll of material. Most reputable HF machine suppliers (like me, for example) will let you send in a sample of your material and test it for free before you commit. That’s a game-changer—why waste money on a machine that can’t handle your stuff?
I’ve also seen mistakes with thickness in the other direction. Someone had a 5mm vinyl for a truck tarp, tried to use a 1.5kW machine, and the heat never penetrated all the way through, so the seal fell apart in the first rain. That’s why matching your machine power to both material thickness and application is key.
So to wrap up the general minimums I tell all my customers:
- 0.08mm to 0.15mm: Super thin films, hobbyist projects, small decorative seals. Use a 1kW to 1.5kW tabletop HF press.
- 0.15mm to 1mm: Flexible PVC/PU for inflatables, decals, medical drapes. Use a 1.5kW to 2.5kW machine.
- 1mm to 5mm: Rigid vinyl, tarps, car trim, packaging. Use a 2.5kW to 5kW heavy-duty machine.
- Anything over 5mm: Industrial applications, large parts, high-powered (5kW+) machines.

But here’s the thing—these are just guidelines. The best way to know for sure is to run a test with your actual material and machine. Every material is a little different, and every machine has its own sweet spot. If you’re not sure which machine is right for your minimum thickness needs, or you want to test a sample to make sure the seal is strong enough, reach out. I’ve helped hundreds of customers pick the right machine for their specific projects, no pushy sales talk, just straight-up advice.
Urine Bagblood Bag Production Line Don’t waste time and money guessing—get the right machine for your thickness needs. Contact us to discuss your welding requirements, request a sample test, or get more info on HF machines tailored to your work. You can check what machines we offer for thin and thick materials, but don’t hesitate to message if you have questions.
Dongguan Yongjia Machinery Equipment Co., Ltd.
We are one of the most reliable hf welding machine manufacturers and suppliers in China, specialized in providing high quality customized service. Please feel free to wholesale advanced hf welding machine at low price from our factory. For quotation, contact us now.
Address: No. 240, Chashan South Road, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: info@yjwelding.com
WebSite: https://www.yjhighfrequencymachine.com/
